Pneumatic Vibrator
Compressed air instead of a motor, so it runs in dusty and hazardous areas, and the force is trimmed at the regulator rather than at the panel.
Compressed air driven
Adjustable force
For hazardous areas
Multiple mountings
Powered by
Compressed air
Adjustment
Force and frequency, through air pressure
Fitted to
Silos, bins, hoppers, chutes, feeders and conveyors
Best for
Dusty and hazardous areas where an electric unit is not suitable
Where an Electric Vibrator Should Not Go
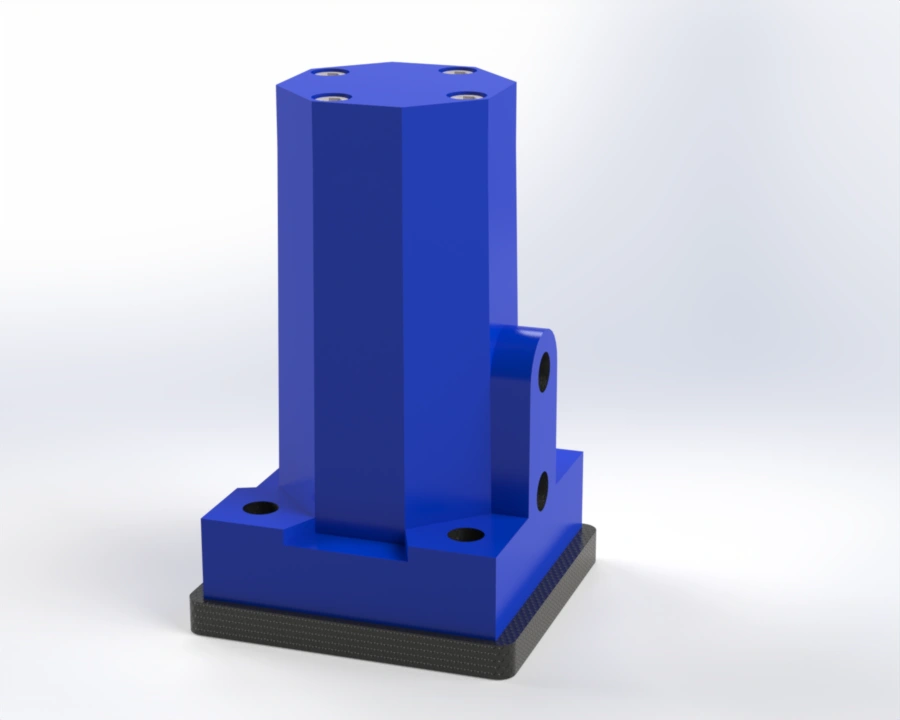
Cosben Engineering’s pneumatic vibrator is designed to improve material flow and reduce common issues like bridging, rat-holing, sticking, and material build-up in bulk handling systems. In silos, hoppers, and bins, such problems can interrupt operations – this is where a reliable air vibrator or hopper air vibrator becomes essential.
Powered by compressed air, this industrial pneumatic vibrator delivers consistent vibration performance even in dusty or hazardous environments where electric solutions may not be suitable. It is widely used across industries handling powders and bulk solids, helping maintain steady discharge and smoother process flow.
From silos and chutes to feeders and conveyors, Cosben pneumatic vibrators support efficient material movement while reducing the need for manual intervention.
At a Glance
Powered by
Adjustment
Fitted to
Best for
Key Features & Benefits
Four points, and the deciding one is where it is allowed to be installed.
01
Effective Flow Aid
Helps eliminate bridging, rat-holing, and material build-up.
02
Suitable for Harsh Environments
Compressed air operation makes it ideal for dusty and hazardous conditions.
03
Consistent Performance
Ensures stable material discharge across continuous operations.
04
Flexible Installation
Compact design allows easy integration into existing systems.
Next Step
Talk to Our Engineers
Share your material, duty and layout and we will size it for your process.
Salient Features
A short list of what the housing, the mounting and the air control give you.
- Compressed air–operated vibrator suitable for hazardous and dusty environments
- Robust industrial-grade housing designed for continuous duty operation
- Effective flow aid for powders, granules, and bulk solids
- Adjustable vibration force and frequency through air pressure control
- Compact and lightweight design for easy integration into existing equipment
- Low maintenance construction with long service life
- Energy-efficient operation with minimal operating costs
- Low noise level compared to conventional electric vibrators
Related Equipment
Often specified alongside this equipment to move and filter material downstream.
Screw Conveyor
Bin Activator