Cosben

Ground Mounted Dust Collector (Vibratory Type)

Ground Mounted Dust Collector (Vibratory Type)

Centralized dust control for multi-silo installations, cleaning cartridges mechanically so no compressed air line is needed, with collected dust returned to the process.

Silos Up to 4

Tons · 25 to 250

FIltering Offline cleaning

Cleaning No compressed air

Served

Silos

Up to 4

Tons

Silo

25 to 250

Filtering

High Efficiency

Offline cleaning

Type

Cleaning

No compressed air

Built to Vent Four Silos From One Filter

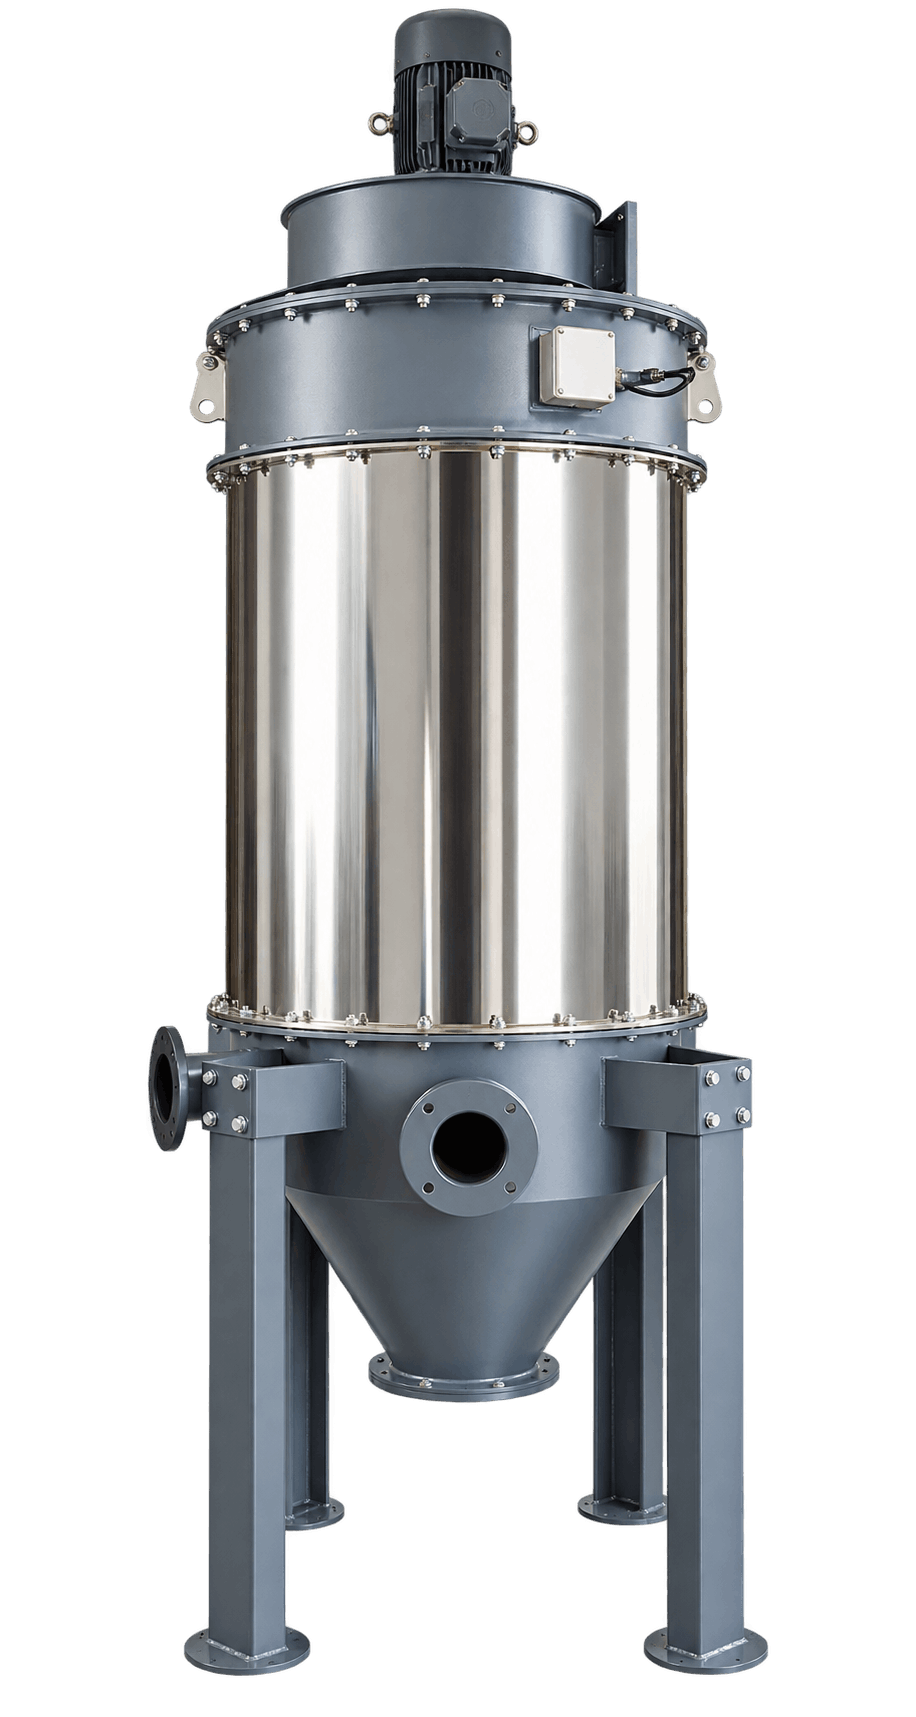
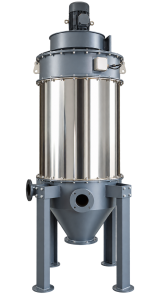
Cosben Engineering’s ground mounted dust collector (vibratory type) is designed for centralized dust control in applications where more than one silo needs to be handled. In bulk material handling plants, especially where multiple silos operate together, using a single ground mounted dust collector helps simplify dust management while keeping the system cost-effective.

This vibratory dust collector is installed at ground level and can be connected to multiple silos with asynchronous or cyclic dedusting operation. Acting as a practical conveyor dust collector or transfer point dust collector, it helps control emissions while recovering valuable powder materials like cement, fly ash, and microsilica. The collected material is discharged into a hopper below the unit for reuse.

The system uses a mechanical cleaning mechanism that dislodges dust from cartridges without compressed air. As an industrial vibratory dust collector, it is designed for offline cleaning and is used for venting one silo at a time

At a Glance

Silos served

Up to four, asynchronous or cyclic dedusting

Silo capacity

25 to 250 tons

Recovery

Cleaning Mechanical vibratory cleaning, no compressed air required

Recovery

Collected dust stored in a hopper for reuse in the process

Key Features & Benefits

Why plants without a compressed air line specify the vibratory collector.

01

Centralized Dust Control

Supports dust collection from multiple silos through a single system.

02

Vibratory Cleaning Mechanism

Mechanical cleaning of cartridges without the need for compressed air.

03

Material Recovery System

Material Recovery System

04

Cost-Effective Solution

Reduces the need for individual dust collectors on each silo.

Next Step

Talk to Our Engineers

Share your bag size, material and layout for a plant-specific recommendation.

Salient Features

One filter body at ground level, cleaned mechanically rather than pneumatically.

Ground Mounted Filter

Technical Specifications

Baseline configuration. Airflow is confirmed against the number of silos and the duty.

GROUND MOUNTED DUST COLLECTOR (VIBRATORY)
Model : Ground Mounted Dust Collector
(Vibratory Type)
Air Volume
Can handle up to 1500 m3/Hr
Filtration Area
23 m2
Dust Particle handling capacity
> 10 microns
Temperature
10° C - 150° C
Outlet Emission
50 mg/nm3

Installations & Applications

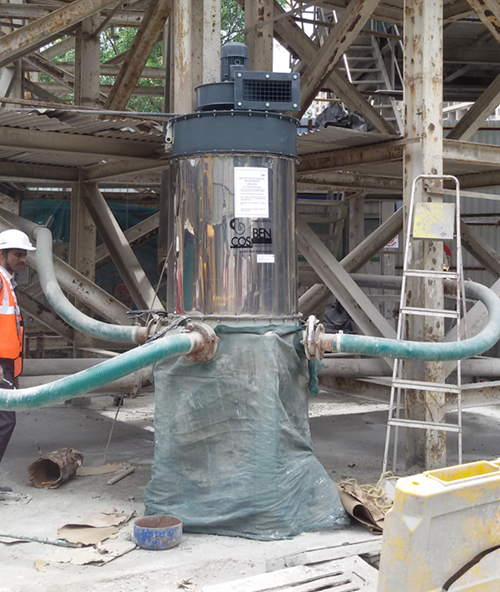
Ground mounted dust collector (vibratory type) supplied and commissioned by Cosben Engineering, shown in the plant conditions they are built for.

Weigh Hopper
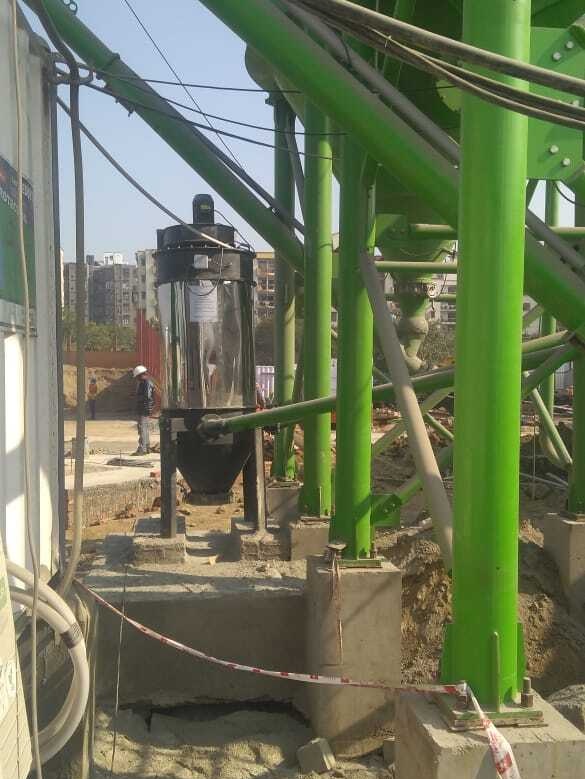
Installations & Applications of Ground mounted dust collector (Vibratory Type) at Lower Parel Site
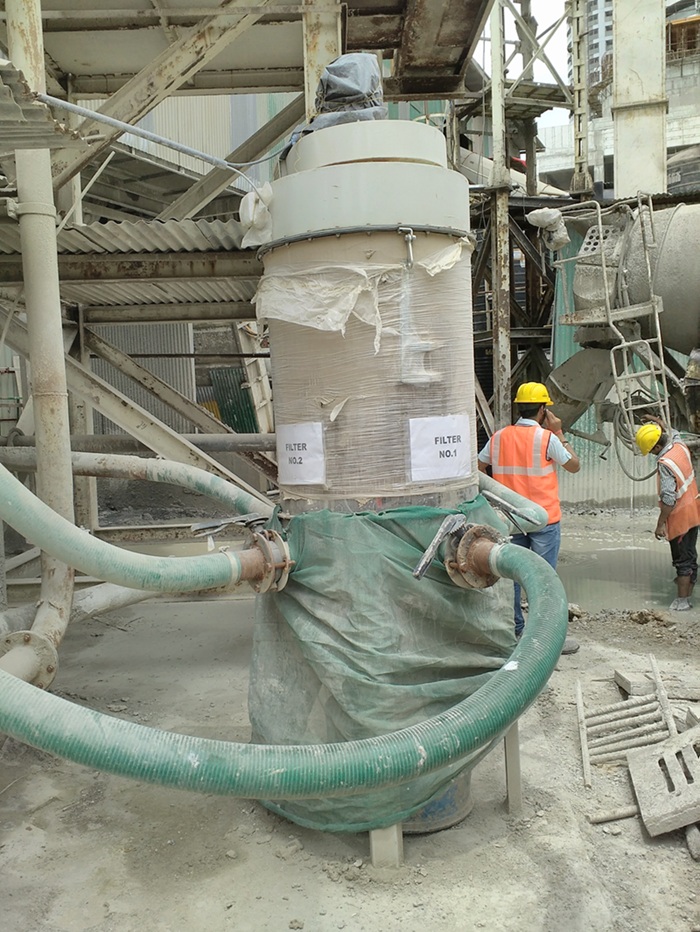
Dust Conditioner installation 2
Installations & Applications of Ground mounted dust collector (Vibratory Type) at Hinjewadi Site
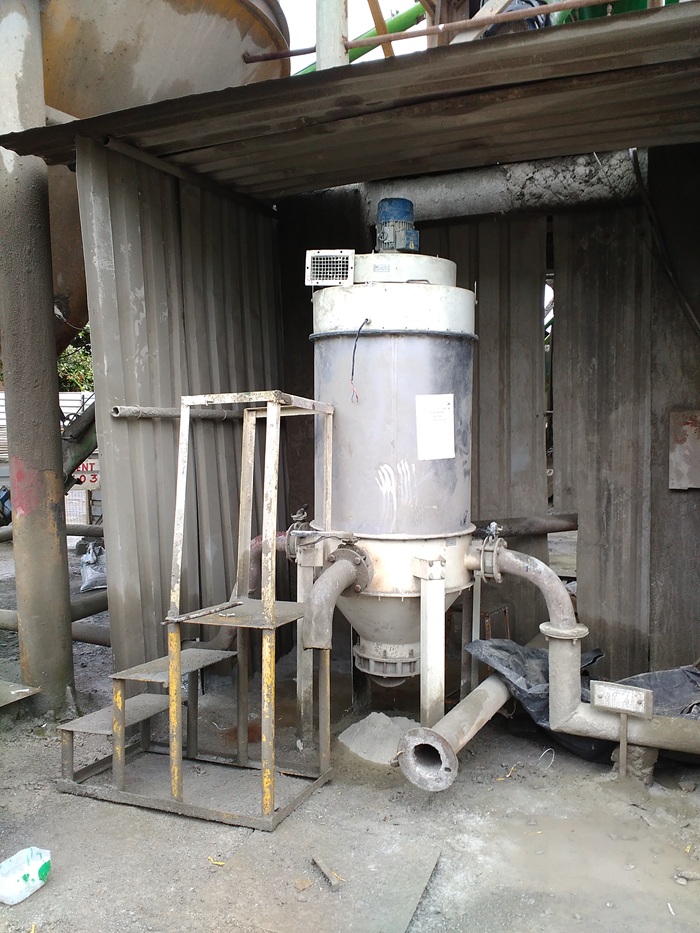
Dust Conditioner installation 3
Installations & Applications of Ground mounted dust collector (Vibratory Type) at Gaziabad Site
Weigh Hopper
Installations & Applications of Ground mounted dust collector (Vibratory Type) at Manglore Site
Related Equipment

Often specified alongside the bag dumping station to move and filter material downstream.

Screw Conveyor

Screw Conveyor

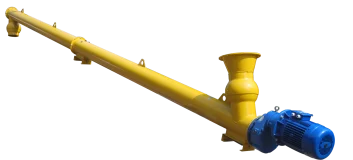
Transfers dumped material onward from the hopper outlet to the next process stage.
bin-activator2

Bin Activator

Vibratory flow aid that prevents arching, rat-holing and material build-up at the hopper outlet below the dumping station.
Butterfly Valve

Butterfly Valve

Manual or pneumatic flow-control valve for isolating and regulating discharge from the hopper below the station.
Scroll to Top