#Aboutindustry
Reliable chemical production begins with consistent material handling. Before raw materials reach reactors, mixers, blending systems or packaging lines, powders and bulk solids must be received, stored, conveyed, weighed, dosed and transferred safely while maintaining process consistency and minimizing product loss.
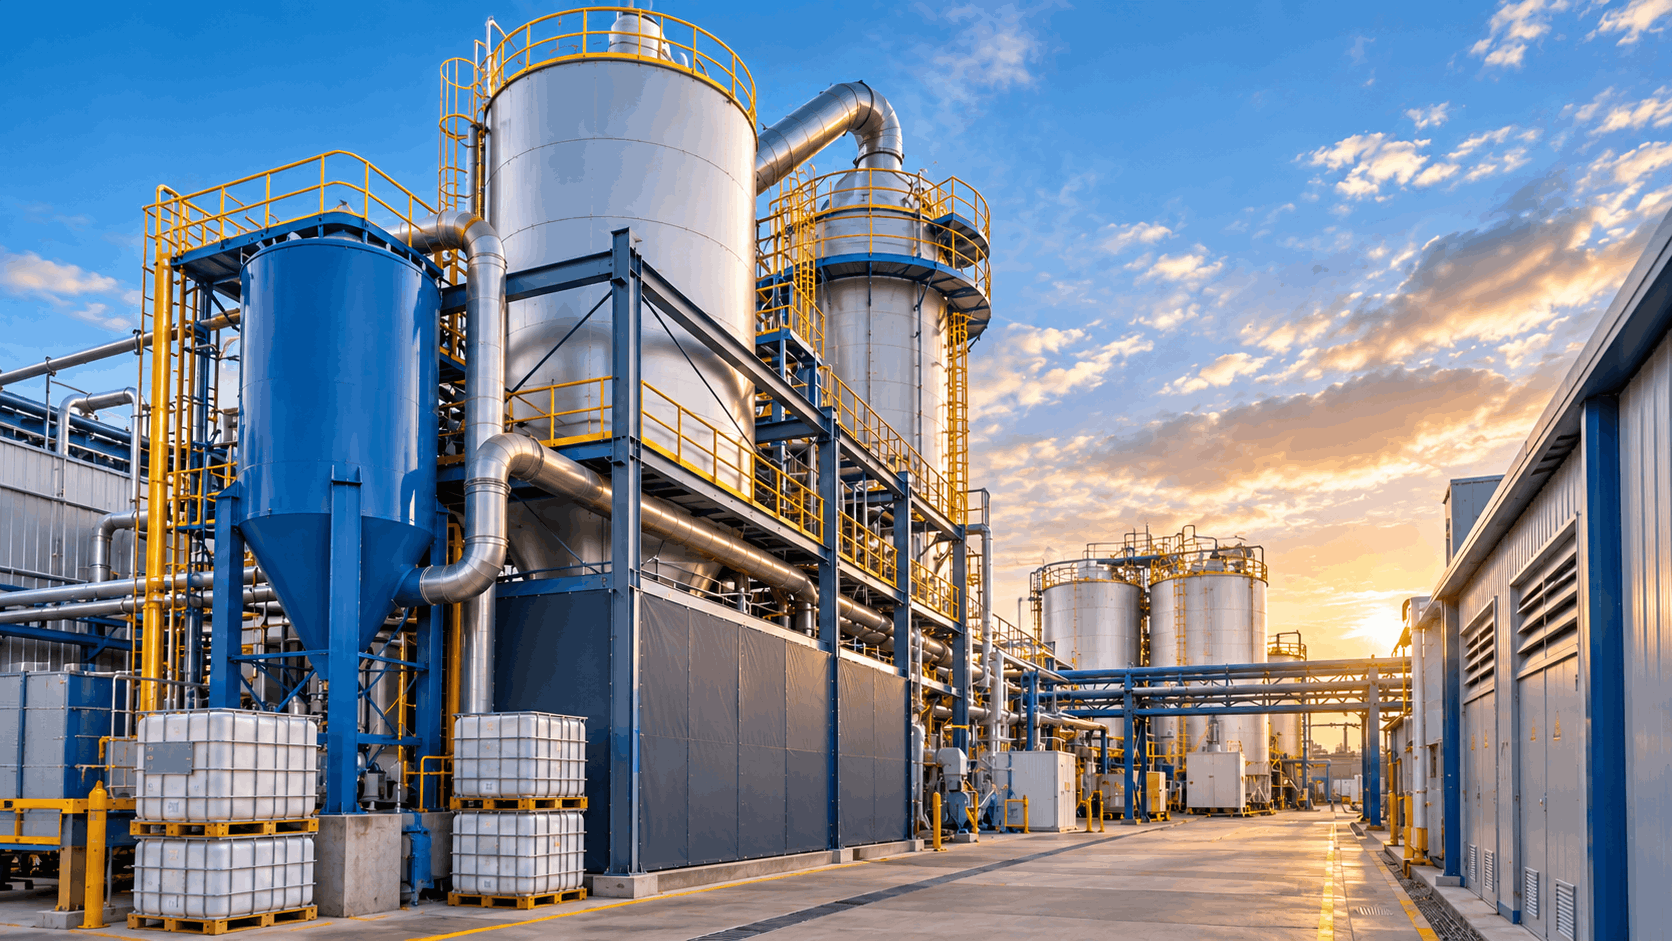
Bulk Material Handling Solutions for Chemical Processing Plants
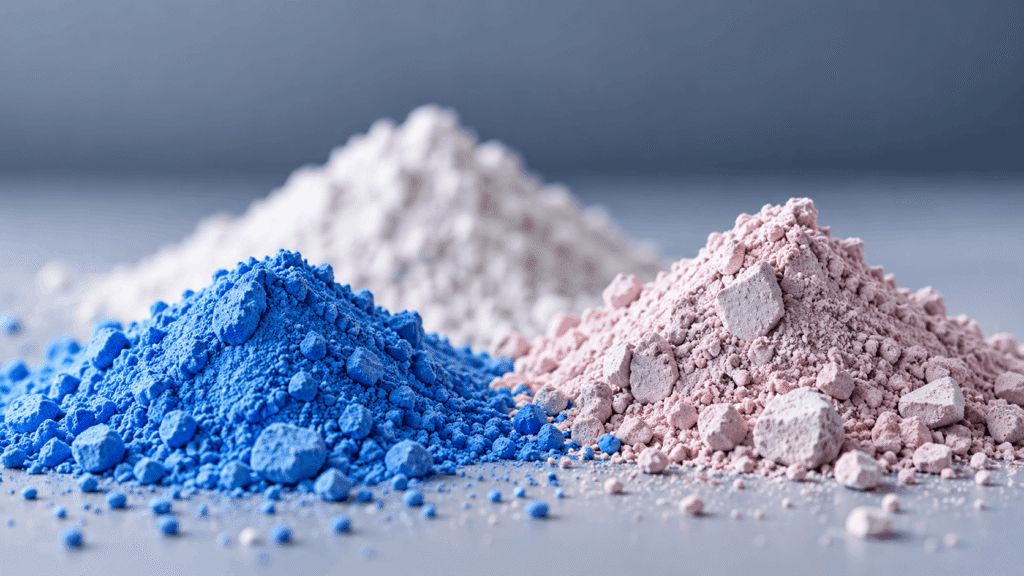
Chemical manufacturing plants process a wide range of powdered and granular materials including pigments, carbon black, titanium dioxide, soda ash, fillers, specialty chemicals, polymer additives, mineral powders, catalysts and functional ingredients. These materials often differ significantly in particle size, bulk density, flow characteristics and dust generation, making engineered material handling essential throughout the manufacturing process.
READ MOREModern Chemical Material Handling Solutions require far more than standalone equipment. Manufacturers need integrated systems that maintain controlled material flow, accurate dosing, reliable storage, efficient conveying and effective dust management while supporting consistent batch production and dependable plant operation.
As an OEM manufacturer, Cosben Engineering Pvt. Ltd. designs and manufactures complete material handling systems for chemical processing facilities. Our engineered solutions include chemical powder conveying systems, chemical feeder and conveyor systems, chemical storage silo solutions, conveying equipment, feeders, dust collection equipment and material flow control solutions that integrate seamlessly with modern chemical manufacturing plants.
Every system is engineered according to material characteristics, production capacity and plant layout. Whether manufacturing specialty chemicals, construction chemicals, industrial chemicals, pigments, resins, masterbatches or powdered additives, Cosben delivers customized engineering solutions that improve material flow, reduce downtime, maintain process consistency and support reliable long-term production.
#Commonchallenges
Common Material Handling Challenges in Chemical Processing Plants
Chemical manufacturing depends on accurate and reliable movement of powdered and granular materials throughout every production stage. Interruptions in conveying, inaccurate dosing, poor blending, excessive dust or inconsistent feeding can directly affect batch quality, production efficiency and operational reliability. Chemical manufacturers commonly experience:
Maintaining Consistent Powder Flow Throughout Chemical Production
Chemical manufacturing requires continuous and controlled movement of powders between storage, batching, blending, mixing and downstream processing equipment. Interruptions in material flow can affect production efficiency, batch consistency and plant reliability.
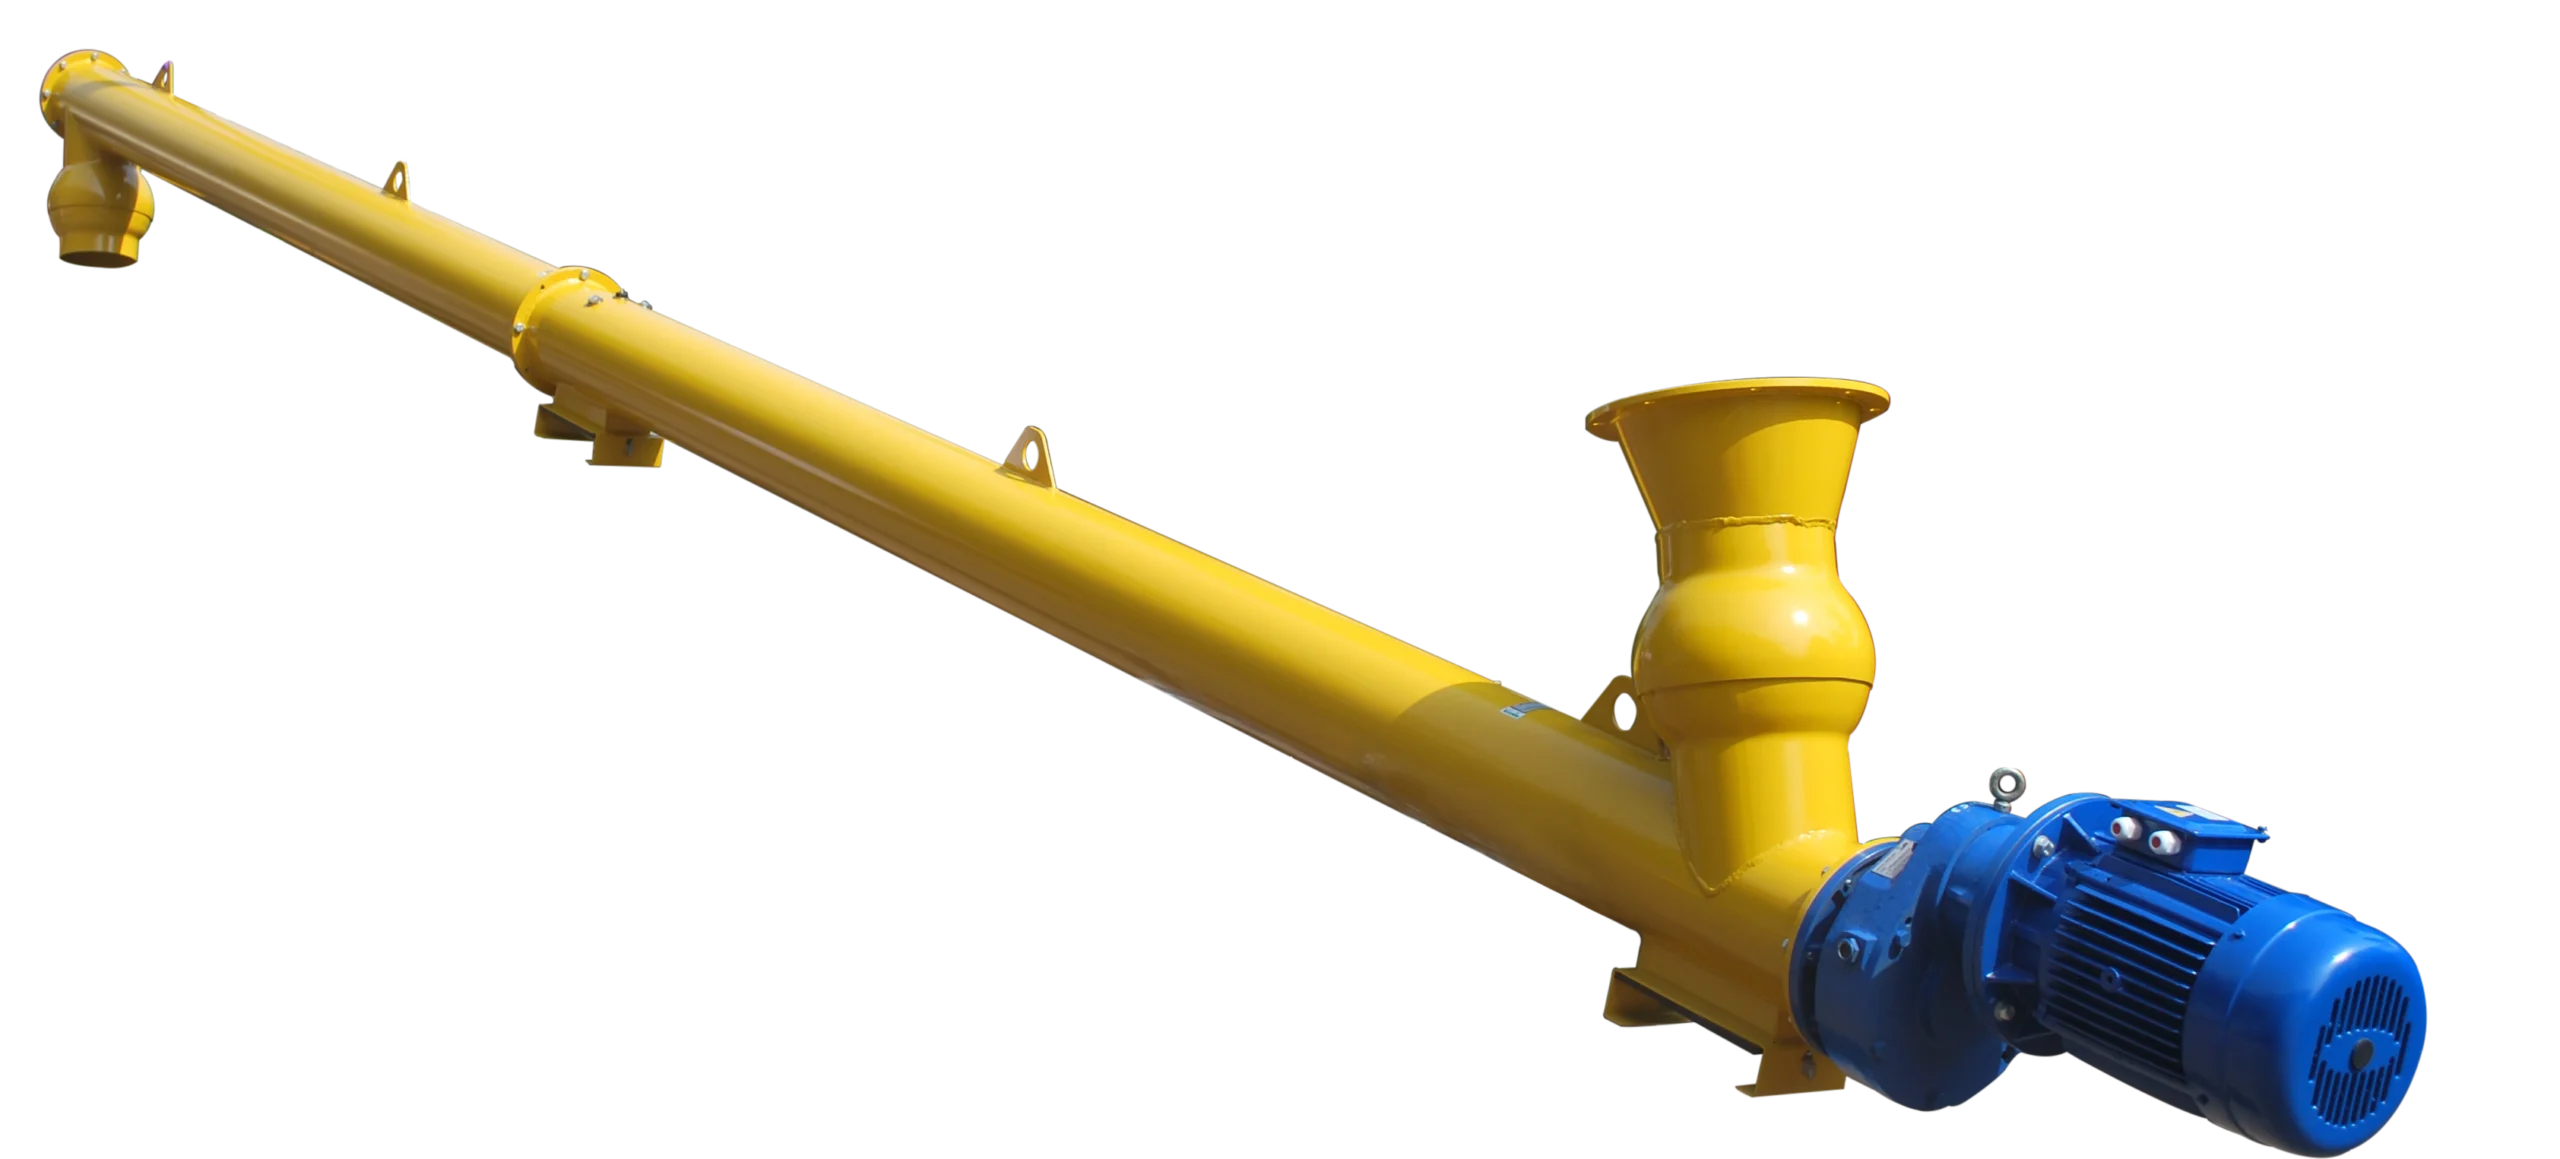
Cosben Engineering develops complete Chemical Material Handling Solutions that maintain reliable powder movement throughout the production process. Our customized chemical powder conveying systems, chemical conveying systems and chemical feeder and conveyor systems are engineered according to material flow characteristics, conveying distance, production capacity and plant layout to ensure dependable transfer of powders and bulk solids across every stage of manufacturing.
Whether supplying blending systems, batching stations, reactors or packaging lines, our engineered conveying solutions improve process stability while reducing unnecessary material handling and product segregation.
Recommended Equipment
Reducing Dust During Chemical Powder Handling
Many chemical raw materials generate fine airborne dust during unloading, conveying, batching, blending and silo filling. Besides material loss, excessive dust increases housekeeping requirements, affects equipment reliability and may reduce workplace safety depending on the material being handled.
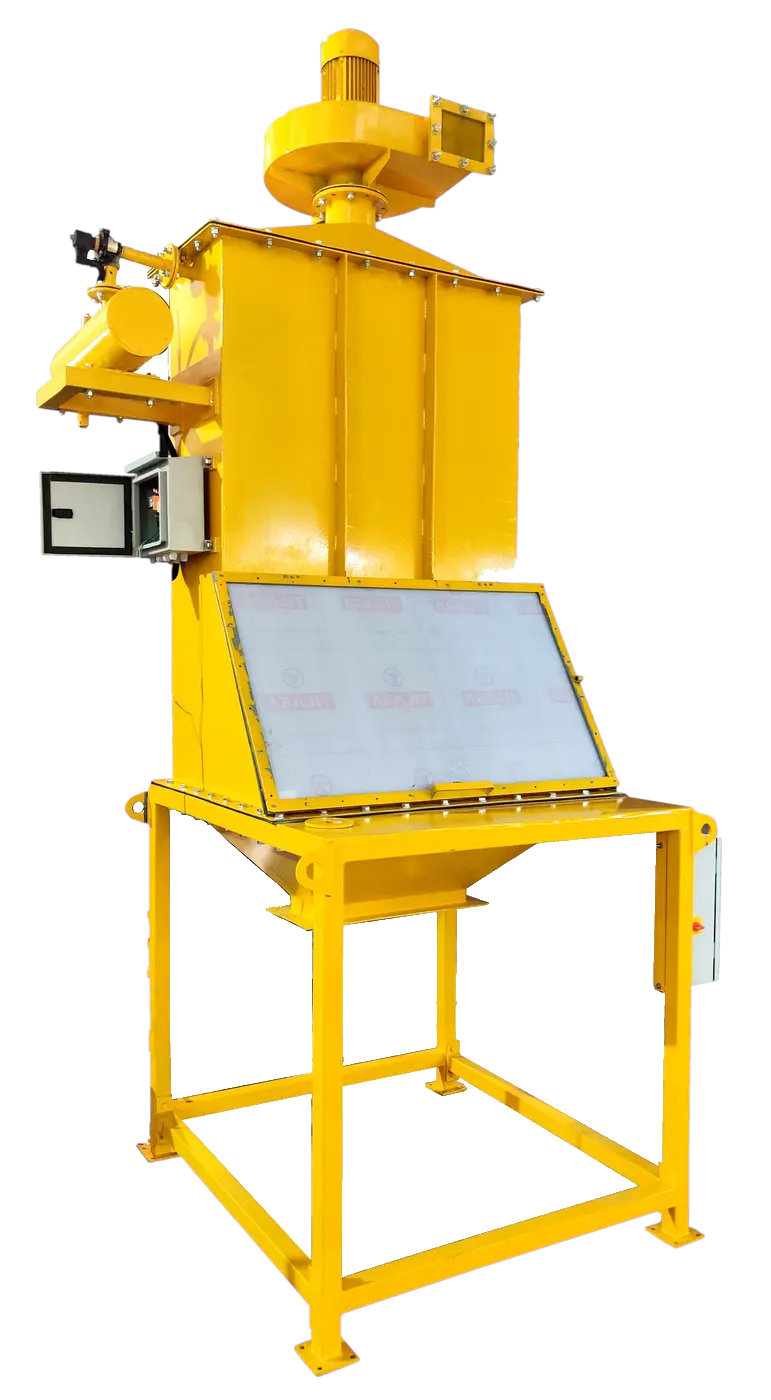
Cosben designs integrated chemical dust collection equipment that minimizes dust generation throughout powder handling operations. Combined with enclosed conveying systems, sealed transfer points and engineered discharge arrangements, our solutions help improve housekeeping while supporting better product recovery and cleaner production environments.
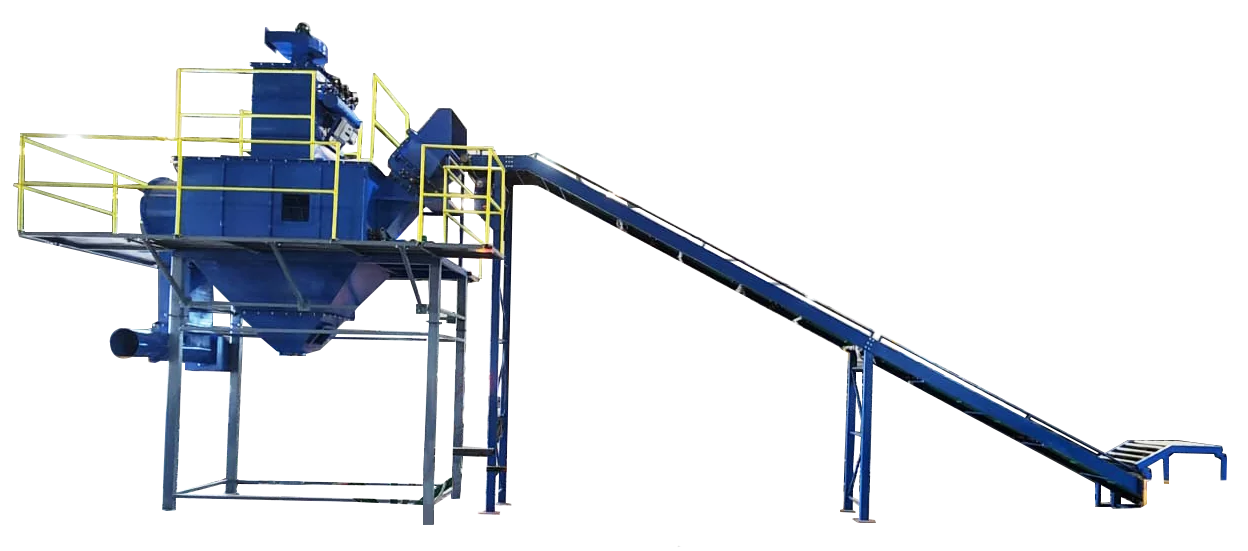
Where raw materials are received in bags or FIBCs, our unloading systems reduce manual handling while improving dust containment during material transfer.
Recommended Equipment
Ensuring Reliable Chemical Storage & Material Discharge
Chemical powders often exhibit varying flow behaviour depending on particle size, moisture absorption, bulk density and storage conditions. Poor discharge from silos and storage hoppers can interrupt production, reduce batching accuracy and increase manual intervention.
Cosben engineers dependable chemical storage silo solutions and chemical storage and conveying systems that maintain controlled material discharge under varying operating conditions. Through optimized hopper geometry and application-specific flow aids, our systems improve chemical plant material handling while supporting reliable material transfer between storage, conveying, batching and downstream processing equipment.
Stable material discharge improves production continuity while maintaining consistent raw material availability throughout the manufacturing process.
Recommended Equipment
Achieving Accurate Chemical Batching & Ingredient Dosing
Many chemical products are manufactured using carefully controlled formulations where each raw material contributes to the final product's performance. Whether producing construction chemicals, pigments, specialty chemicals, polymer additives, detergents or industrial compounds, accurate weighing and ingredient dosing are essential for maintaining consistent product quality.
Cosben Engineering develops integrated chemical dosing and blending systems that support reliable material preparation before downstream processing. Combined with engineered conveying and feeding equipment, our systems deliver controlled material flow to batching stations, helping manufacturers maintain formulation consistency while minimizing material losses and production variability.
Our customized chemical batch mixing systems and chemical additive dosing systems are engineered according to powder characteristics, batch size, production capacity and plant layout, ensuring dependable operation across a wide range of chemical manufacturing applications.
Recommended Equipment
Improving Powder Blending & Batch Uniformity
Many chemical formulations require multiple powders to be blended uniformly before entering downstream processing equipment. Consistent distribution of pigments, fillers, additives, mineral powders, catalysts or specialty ingredients is critical for achieving repeatable product performance.
Cosben develops material handling systems that support chemical mixing and blending equipment by delivering materials at controlled feed rates while maintaining reliable transfer between storage, batching and mixing operations. Stable conveying and accurate ingredient feeding reduce segregation and improve batch consistency throughout production.
Whether supplying powders to ribbon mixers, plough share mixers, paddle mixers or other chemical processing equipment, our engineered material handling systems improve production reliability while maintaining continuous material flow.
Recommended Equipment
Optimizing Chemical Plant Material Transfer
Modern chemical manufacturing increasingly depends on automated material handling to improve production efficiency, recipe repeatability and process consistency. Integrating storage, conveying, feeding, batching and discharge into one coordinated system reduces manual intervention while improving operational control.
Cosben develops chemical bulk material handling equipment that support chemical process systems across modern manufacturing facilities. Our engineered solutions integrate feeders, conveyors and discharge equipment into a coordinated material handling process designed to improve production stability and simplify plant operation.
Every system is engineered according to material behaviour and plant layout, helping manufacturers improve productivity while maintaining dependable process performance.
Recommended Equipment
Supporting Safe Chemical Ingredient Handling
Chemical plants routinely handle powders that differ significantly in particle size, flowability, bulk density and dust generation. Reliable transfer of these materials between unloading, storage, batching and processing is essential for maintaining production continuity and minimizing unnecessary material losses.
Cosben develops engineered chemical ingredient handling systems and chemical powder feeding systems that provide controlled movement of powders throughout the manufacturing process. Whether handling pigments, fillers, specialty additives or industrial powders, our systems maintain stable material flow while reducing manual handling and improving overall production efficiency.
By engineering equipment according to the behaviour of each material, we help manufacturers achieve consistent feeding and dependable plant performance.
Recommended Equipment
Improving Material Flow Throughout Chemical Production
Reliable chemical manufacturing depends on uninterrupted movement of powders between storage, batching, blending, processing and packaging. Poor conveying performance can lead to inconsistent feeding, material build-up, product segregation and unnecessary production interruptions.
Cosben develops complete powder handling systems for chemical plants that maintain controlled material flow throughout the production cycle. Our engineered conveying, feeding and discharge solutions integrate efficiently with upstream and downstream chemical processing equipment, ensuring reliable transfer while minimizing dust generation and material degradation.
Every system is customized according to powder characteristics, conveying distance, production capacity and process requirements to support long-term operational reliability.
Recommended Equipment
Minimizing Equipment Wear & Production Downtime
Chemical manufacturing facilities often operate continuously while handling abrasive powders, fine chemicals, mineral fillers, pigments and specialty ingredients. Reliable material handling equipment is essential for maintaining production schedules while minimizing maintenance-related interruptions.
Cosben manufactures heavy-duty chemical powder handling equipment using precision engineering, CNC machining, Robotic profile cutting machines and application-specific designs developed for continuous industrial operation. Every system is engineered for dependable performance, simplified maintenance and long service life, supported by genuine OEM spare parts and responsive after-sales service.
Our engineering approach helps chemical manufacturers improve equipment availability, reduce downtime and maintain stable production efficiency.
Recommended Equipment
Preventing Production Downtime with Integrated Chemical Material Handling Solutions
Reliable chemical manufacturing depends on every stage of material handling operating together-from raw material receiving and storage to conveying, feeding, batching, blending and downstream processing. Interruptions in material handling can affect batch consistency, increase production costs and reduce overall plant efficiency.
READ MORECosben engineers complete chemical batching plant solutions that integrate conveying, feeding, discharge and dust control into one coordinated material handling process. Our experienced application engineers evaluate powder characteristics, production capacity and plant layout to develop customized engineering solutions that improve material flow, maintain formulation consistency and support reliable long-term operation.
Supported by in-house engineering, precision manufacturing, CNC machining, Robotic profile cutting machines, installation assistance, genuine OEM spare parts and dependable after-sales support, Cosben helps chemical manufacturers build reliable material handling systems designed for continuous industrial production.
#ProductRange
One Engineering Partner, One Coordinated System
Rather than supplying individual machines, Cosben engineers integrated systems that connect receiving, storage, conveying, feeding, conditioning, discharge and dust control into one coordinated bulk material handling process, supported by in-house engineering, precision manufacturing and genuine OEM spare parts.
#WhyCosben
Why Chemical Manufacturers Choose Cosben Engineering
Chemical manufacturing requires material handling systems capable of maintaining accurate dosing, reliable conveying, controlled storage and consistent batch preparation while operating under demanding industrial conditions.
READ MOREAs an OEM manufacturer, Cosben Engineering develops complete Chemical Material Handling Solutions tailored to each manufacturing process. Instead of supplying individual machines, we engineer integrated systems that connect raw material receiving, conveying, feeding, batching, blending and discharge into one coordinated material handling process.
Why Manufacturers Partner with Cosben
Whether you're expanding an existing chemical plant or developing a new production facility, Cosben delivers engineered material handling systems that improve process reliability, reduce maintenance and support consistent production performance.
Looking for a Complete Material Handling Solution for Your Chemical Plant?
Whether you're manufacturing specialty chemicals, construction chemicals, industrial chemicals, pigments, polymer additives or powdered chemical products, Cosben Engineering provides complete OEM solutions for raw material receiving, conveying, feeding, batching, blending, dust control and bulk material handling.
Our application engineers work closely with your team to understand powder characteristics, production objectives, process requirements and plant layout before developing customized systems that improve material flow, reduce downtime and support consistent product quality.
Connect with Cosben Engineering today to discuss your chemical manufacturing process and discover how our engineered material handling solutions can improve production efficiency, maintain batch consistency and support reliable long-term plant performance.
- OEM engineering, design and in-house manufacturing
- Customized systems engineered around your chemical manufacturing process
- Experienced application engineers specializing in powder and bulk material handling
- Precision manufacturing using CNC machining and Robotic profile cutting machines
- Heavy-duty equipment engineered for continuous industrial operation
- Integrated conveying, feeding, batching, blending and discharge solutions
- Installation guidance and commissioning support
- Genuine OEM spare parts for dependable long-term performance
- Responsive after-sales service and technical assistance
- ISO 9001:2015 certified manufacturing processes
#FAQ
Frequently Asked Questions
What materials can Cosben handle in chemical processing plants?
Our systems are designed to handle pigments, carbon black, titanium dioxide, soda ash, fillers, catalysts, specialty chemicals, polymer additives, mineral powders, construction chemicals, industrial chemicals and other powdered or granular raw materials.
What equipment is required for a complete chemical material handling system?
A complete chemical material handling system typically includes bag unloading equipment, conveyors, feeders, mixing support equipment, dust collection systems and discharge equipment. The final configuration depends on the material properties, production capacity and process requirements.
How do Chemical Material Handling Solutions improve production efficiency?
Integrated Chemical Material Handling Solutions improve powder flow, maintain accurate dosing, reduce manual handling, minimize dust generation and support consistent batch production throughout the manufacturing process.
Can Cosben integrate with chemical processing equipment?
Yes. Cosben's conveying, feeding and discharge systems are designed to integrate with reactors, mixers, blenders, dryers, packaging systems and other downstream chemical processing equipment to ensure reliable material transfer throughout the production process.
Does Cosben manufacture complete chemical processing plants?
No. Cosben specializes in OEM bulk material handling equipment. Our expertise includes conveying, feeding, batching, blending support, discharge systems and dust collection that integrate with process equipment supplied by specialist chemical plant manufacturers.
How do you prevent material bridging inside chemical storage silos?
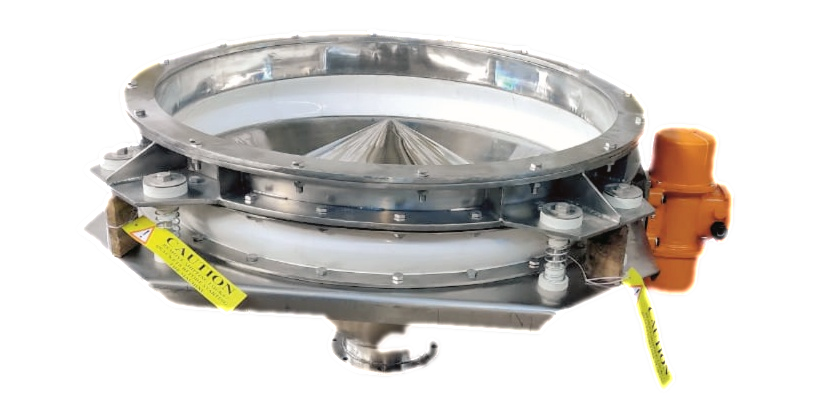
Proper silo design combined with bin aerators, electric vibrators, pneumatic vibrators, butterfly valves and slide gate valves helps maintain reliable powder discharge while reducing manual intervention and improving production continuity.
How is dust controlled during chemical powder handling?
Dust is minimized using enclosed conveying systems, chemical dust collection equipment, sealed transfer points and engineered dust extraction solutions that help reduce airborne dust while improving product recovery.
Do you provide installation and commissioning support?
Yes. Our service team provides supervision for installation, commissioning, operator training and after-sales service to ensure reliable long-term system performance.
Why choose an OEM instead of multiple equipment suppliers?
Working with an OEM provides customized engineering, complete system integration, genuine spare parts, long-term technical support and a single engineering partner responsible for the complete material handling system.